Material Selection for Custom CNC Pipe Fittings
Quick Material Comparison Matrix for Sourcing Engineers
| Material | Machinability | Corrosion Resistance | Pressure Rating | Primary Surface Finish |
| Free-Cutting Brass | Excellent (100%) | High (Freshwater/Oil) | Medium | Natural / Nickel Plated |
| Carbon Steel | Good | Low (Requires Plating) | High to Very High | Clear/Yellow Zinc Plating |
| Stainless Steel (304/316) | Fair | Superior (Acid/Marine) | High | Passivated / Electropolished |
Brass and Copper Alloys
-
Common Applications: Hose barb adapters, pneumatic line connectors, coolant lines, fuel system fittings.
-
Key Advantages: Excellent natural corrosion resistance against water and oil, rapid machining cycle times, clean thread finish without burr buildup.
-
Considerations: Lower tensile strength than carbon or stainless steel; not suitable for extreme pressure lines or high-temperature steam applications without careful wall thickness design.
Carbon Steel
-
Common Applications: Hydraulic bulkhead fittings, heavy-duty threaded plugs, high-pressure hose adapters.
-
Key Advantages: High mechanical strength, excellent resistance to pressure spikes and mechanical vibration.
-
Considerations: Carbon steel requires surface plating to prevent rust. Common post-machining surface treatments include electro-galvanizing (clear or yellow zinc plating) and trivalent chromium passivations. Specify your required salt spray test duration on the drawing to ensure proper plating thickness.
Stainless Steel
-
Common Applications: Chemical processing fittings, marine bulkhead connectors, high-temperature fluid lines.
-
Key Advantages: Superior resistance to pitting, oxidation, and chemical degradation without requiring additional plating.
-
Considerations: Stainless steel work-hardens quickly during machining, resulting in longer cycle times and higher tool wear compared to brass or carbon steel. To manage costs, ensure your draft drawing specifies reasonable tolerances rather than excessively tight figures where standard machining tolerances suffice.
Understanding Thread Standards and Machining Considerations
Tapered Threads: NPT vs. BSPT
-
NPT (National Pipe Taper): Standard in North America. Features a 60° thread angle with flat crests and roots. Taper rate is 1:16.
-
BSPT (British Standard Pipe Taper): Widely used in Europe, Asia, and Commonwealth markets. Features a 55° thread angle with rounded crests and roots. Also has a 1:16 taper rate.
Parallel Threads: BSPP and Metric
-
BSPP (British Standard Pipe Parallel / G-Thread): Uses a 55° thread profile. Often features a sealing chamfer or spot-face on the hex body to accommodate an elastomeric seal.
-
Metric Threads (ISO): Specified by outer diameter and pitch (e.g., M18x1.5). Common in modern automotive, industrial machinery, and European hydraulic equipment. Sealing is typically accomplished via an O-ring boss or captive seal groove machined into the fitting shoulder.
Design for Manufacturability (DFM) Tips for Custom Fittings
-
Standardize Hex Sizes: Design fitting bodies around standard bar stock hex sizes whenever possible. This eliminates the need to mill custom hex flats on round bar stock.
-
Include Thread Relief Grooves: Provide adequate undercut or thread relief space between the last full thread and an adjacent shoulder to allow smooth tool run-out during CNC thread turning.
-
Chamfer Lead-Ins: Specify a 45° chamfer on the leading thread edge. This protects the first thread from damage during shipping and helps operators align fittings during manual assembly.
How Hongqian Handles Your Custom CNC Orders
Frequently Asked Questions
Ready to Start Your Custom CNC Machining Project?
-
2D or 3D drawing (PDF, STEP, or IGES)
-
Material grade (e.g., Brass C36000, Carbon Steel, SS304/316)
-
Thread specification & tolerance callouts
-
Surface finish / plating requirements (e.g., Yellow Zinc, Passivation, Plain)
-
Target order quantity
Frequently asked questions
01Do you sell standard off-the-shelf pipe fittings from a catalog?
No. We operate strictly as an OEM/ODM CNC machining factory. We produce custom pipe fittings, hose barb adapters, bulkhead connectors, and threaded plugs built exclusively to customer drawings and specifications.
02What information is required to get an accurate price quote?
To provide a detailed quote, please send a 2D drawing (PDF with dimensions and thread specs) or 3D CAD file (STEP/IGES), required raw material grade, surface finish/plating requirements, and estimated order quantity.
03Can you machine custom threads that differ from standard NPT or BSP?
Yes. Because we machine components on multi-axis CNC lathes using programmed thread cycles, we can cut custom pitch, non-standard metric threads, or specialized modified threads. Specific gage requirements should be confirmed on your drawing or RFQ.
04What is your typical lead time for custom fitting samples?
For custom CNC machined fittings requiring standard raw material bar stock, sample lead times are typically around 10 working days, subject to specific drawing complexity and post-machining surface treatment requirements.
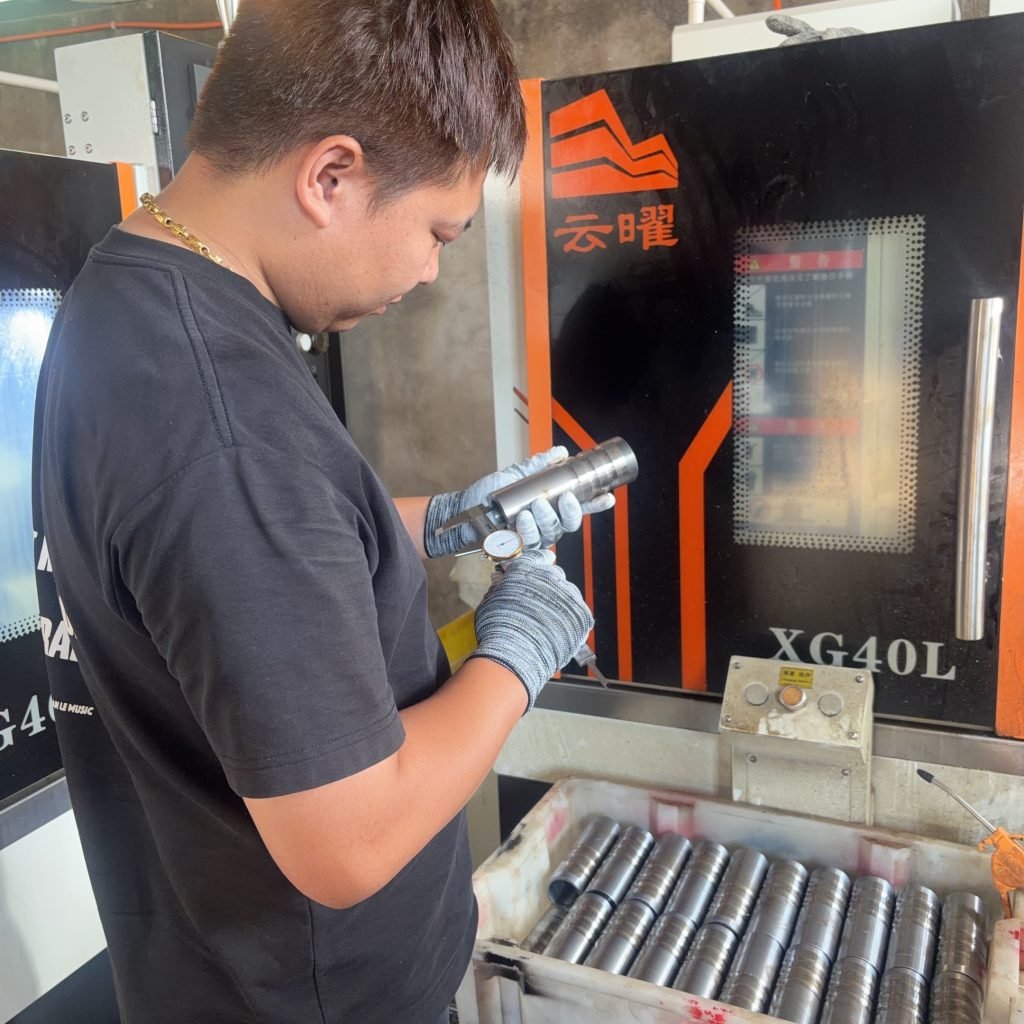
05How do you verify thread accuracy on custom orders?
We inspect threads during setup and throughout production runs using calibrated Go / No-Go thread plug and ring gages corresponding strictly to the specified thread standard (NPT, BSPT, BSPP, or Metric) on your drawing.