The Hidden Risks of Relying Solely on Standard Part Factories
-
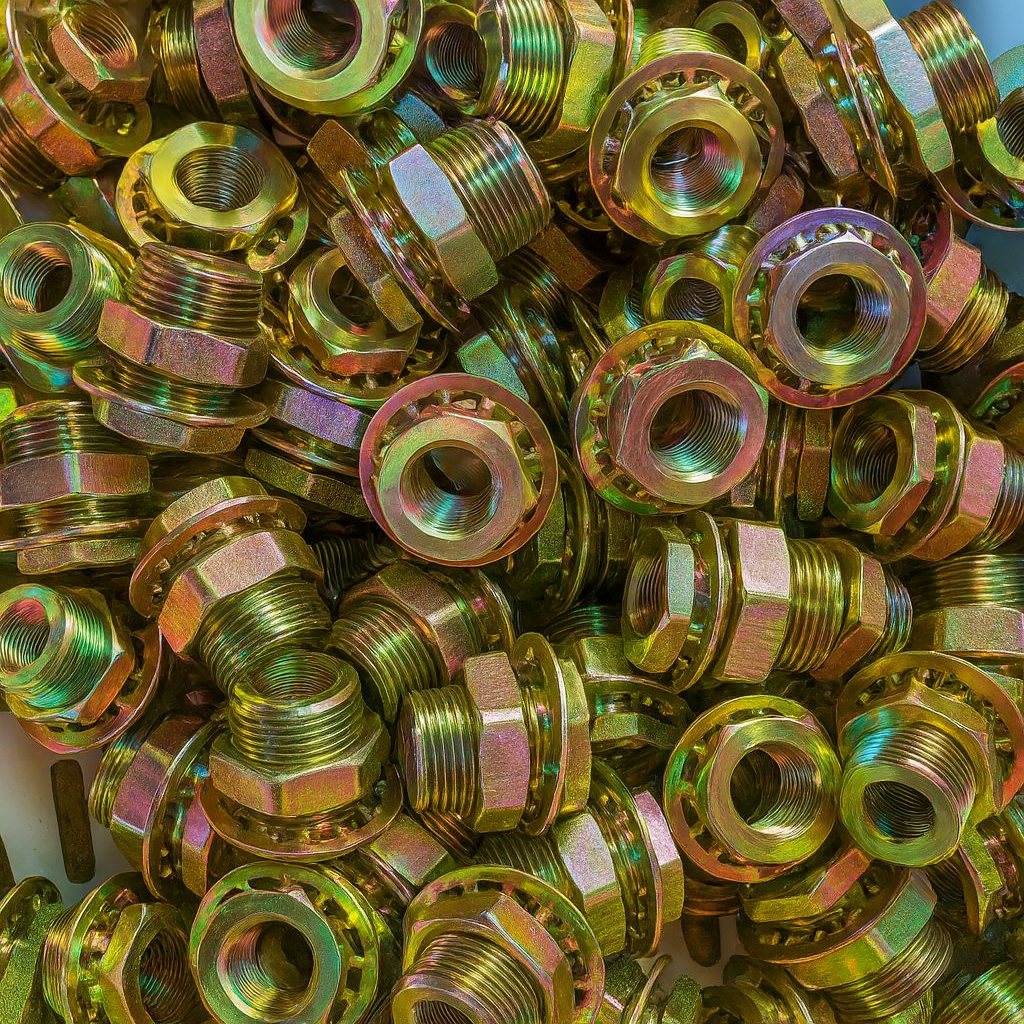
Aluminum Anodizing Blanks: When producing aluminum fittings or adapters intended for bright or hard anodizing, you must select solid bar stock or hot-forged blanks. Using ordinary hollow tubing often leaves subsurface press marks and structural defects that ruin the finish after anodizing.
-
303 Stainless Steel Electrolytic Polishing: High-sulfur alloys like 303 stainless steel cannot be effectively electropolished. Their high sulfur content routinely creates unsightly streak lines instead of a clean, uniform polish.
-
Medium Carbon Steel Cold Heading: Forming fasteners or plugs from medium carbon steels like AISI 1045 (45# steel) via cold heading requires proper intermediate annealing or tempering heat treatment beforehand. Without it, high stress leads to immediate cracking and structural failure.
Core Advantages of an Integrated Custom Machining Facility
-
Broad Process Versatility: Comprehensive management of turning, threading (including NPT, BSPP, BSPT, Metric, and UNF standards), punching, and custom laser or stamp marking.
-
Rigorous Quality Verification: Strict inspection protocols utilizing calibrated Go/No-Go plug and ring gauges, profile projectors, and detailed dimensional and material test reports.
-
Material Flexibility: Processing round bars, hollow tubing, hex stock, hot forgings, and precision castings across various carbon and stainless steel grades.
Surface Treatments Tailored to Alloy Properties
Frequently Asked Questions
-
What is the main benefit of choosing a non-standard custom fittings supplier?Non-standard custom factories prioritize equipment and process diversity. By handling everything from blanking and CNC turning to threading, optical inspection, and test reporting under one roof, we eliminate subcontractor friction and prevent metallurgical errors common in standard catalog production.
-
Why does raw material selection matter for surface treatments like aluminum anodizing?For anodized aluminum parts, using solid bar stock or hot forgings prevents the structural press marks and surface defects frequently caused by standard hollow tubing.
-
Can 303 stainless steel be electropolished?No. Because 303 stainless steel has a high sulfur content to improve machinability, electrolytic polishing will result in streak lines rather than a smooth finish.
-
What thread standards can your facility machine?We routinely machine standard international thread geometries including NPT, NPTF, BSPP, BSPT, Metric, UNF, and UNEF, verified using calibrated pitch diameter gauges.
-
What is the typical sample and production lead time?Sample lead times typically take around 10 working days. Full production schedules depend on part complexity and order volume—please submit your blueprint for an exact quote.
-
How do I request a custom quotation?You can send your 2D/3D CAD drawings, material specs, thread requirements, surface finishes, and estimated quantities directly through our Contact Page.
Frequently asked questions
01What is the main benefit of choosing a non-standard custom fittings supplier?
Non-standard custom factories prioritize equipment and process diversity. By handling everything from blanking and CNC turning to threading, optical inspection, and test reporting under one roof, we eliminate subcontractor friction and prevent metallurgical errors common in standard catalog production.
02Why does raw material selection matter for surface treatments like aluminum anodizing?
For anodized aluminum parts, using solid bar stock or hot forgings prevents the structural press marks and surface defects frequently caused by standard hollow tubing.
03Can 303 stainless steel be electropolished?
No. Because 303 stainless steel has a high sulfur content to improve machinability, electrolytic polishing will result in streak lines rather than a smooth finish.
04What thread standards can your facility machine?
We routinely machine standard international thread geometries including NPT, NPTF, BSPP, BSPT, Metric, UNF, and UNEF, verified using calibrated pitch diameter gauges.
05What is the typical sample and production lead time?
Sample lead times typically take around 10 working days. Full production schedules depend on part complexity and order volume—please submit your blueprint for an exact quote.
06How do I request a custom quotation?
You can send your 2D/3D CAD drawings, material specs, thread requirements, surface finishes, and estimated quantities directly through our Contact Page.